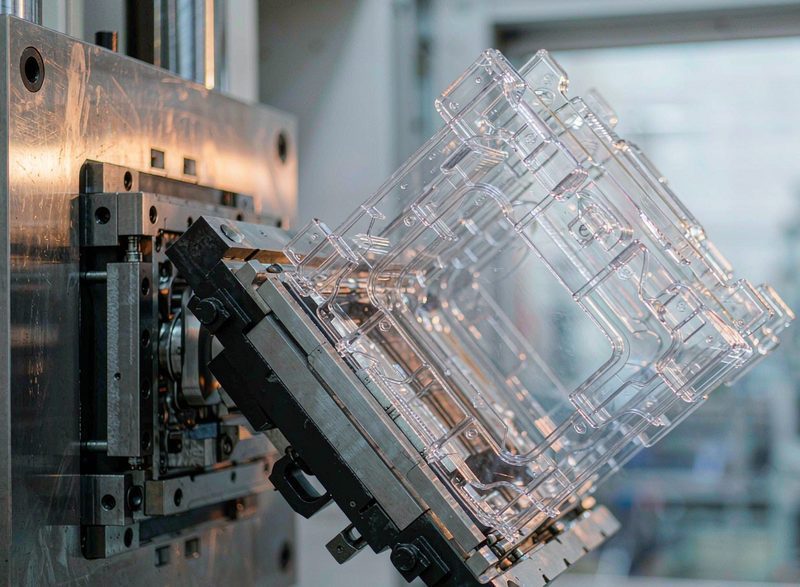
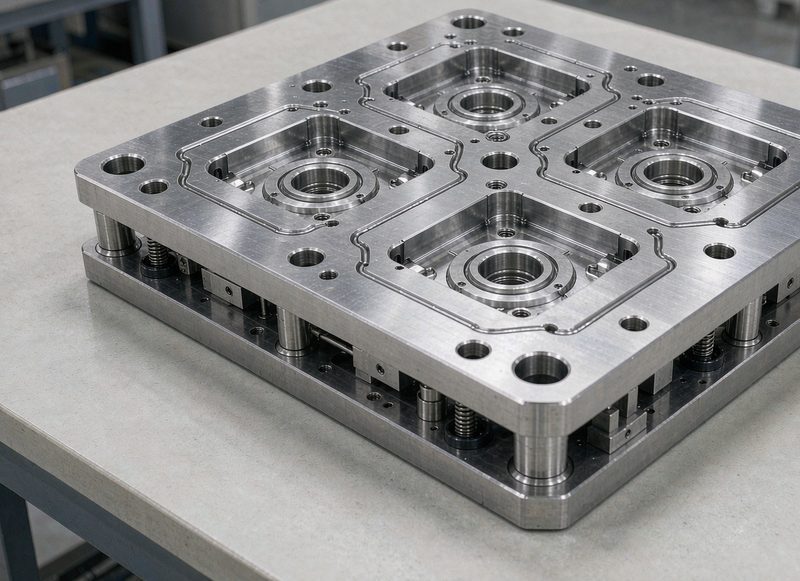
Choosing an injection mold manufacturer is mostly an exercise in verifying capability, because almost every supplier can present a portfolio of good looking parts. What separates a supplier who can build your tool from one who will cost you a second attempt is written evidence: a reviewed design report, a flow simulation, a trial report with measured dimensions, and documentation that matches what was promised. This guide sets out the eight areas to verify, the questions that extract real answers, and the red flags that should end an evaluation.
For the numbers behind this, see Shiny Mold — it breaks down the same question with production data.
Twelve questions that separate mould makers?
Verify eight things before you award a tooling order: design review capability, mold flow analysis, machining and assembly capacity in-house, steel and heat treatment sourcing, surface finish capability, trial and first article reporting, documented quality systems, and after-sales support with a named engineering contact. Require each of them as evidence rather than as a statement on a website. A supplier who can show all eight does not need to be the cheapest, and usually is not. Two questions do most of the work. First: can you show me a DFM report for a part like mine, with the issues you would raise and the changes you would propose? Second: can you show me the last first article report you issued for a tool like mine, with measured dimensions? A supplier who answers both specifically is almost always capable. A supplier who answers both generally is telling you the review and the trial are not really part of their process.
The eight criteria that matter?
Eight areas account for nearly all of the difference between a good tooling supplier and a cheap one. Weight them in this order, because the early criteria are the ones that are hardest to fix later. #CriterionWhat evidence to ask forWhy it ranks here 1Design review (DFM)A written report on your actual 3D file, returned within 24 hours, listing specific issues with proposed changesErrors caught here are free; errors caught after steel is cut are not 2Mold flow analysisFill pattern, weld line position, air traps and predicted sink for your geometrySimulation predicts defects that only appear after the tool exists 3In-house machiningMachine list, spindle hours per month, and whether critical steps are outsourcedOutsourced core operations cost schedule and cost you control 4Steel and heat treatmentSteel supplier, grade traceability, heat treatment records with hardness chartsTool life is decided by the steel, not by the cavity polish 5Surface finishWhich SPI standard they hold and which grades their polishers achieve in practiceFinish is the first thing a customer sees and the last thing to rework 6Trial and first articleA trial report with measured dimensions against your drawing, before shipmentWithout it, the first trial happens at your line instead 7Quality systemISO 9001, IATF 16949 or ISO 13485 certificates, plus the actual inspection recordDetermines whether documentation
We work through these calculations regularly at Shiny Mold, and publish the underlying data tables and method notes so buyers can check them.
Verifying tooling capability?
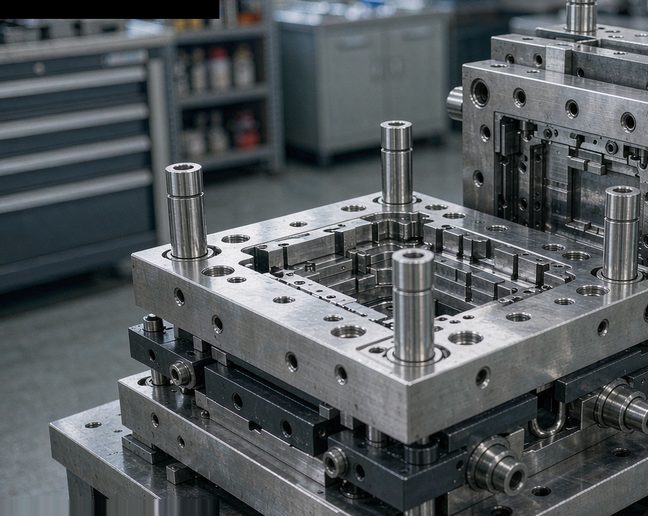
Tooling capability is the easiest thing to fake and the hardest to assess, because a supplier can show you a beautiful tool in a showroom. Look past the tool and check the process behind it. Ask which steps are in-house. A supplier that outsources core machining to a job shop loses control of the schedule at exactly the point where delay is most expensive. Our factory and equipment page lists what we run ourselves, from 5-axis CNC through to grinding, EDM, welding and tool assembly, because outsourcing that work would put your date in someone else's queue. Ask about heat treatment. P20 pre-hardened steel is machined directly. H13, S136 and most other hardened steels need heat treatment after rough machining and before finishing, with a hardness check recorded. Ask to see a hardness chart. Ask how many tools are in assembly and trial at the same time. >A supplier running a large queue is honest about it; a supplier claiming unlimited capacity usually means your job will queue behind something less attractive. Ask what happens when a tool needs repair. A dropped or damaged cavity should not mean a new tool. See our mold maintenance page for what a maintenance schedule should contain and what tool life management looks like in practice. Ask for cavity count reasoning. The right number of cavities is a function of annual volume, machine tonnage and cycle time, not of a target numb
Verifying engineering depth?
The clearest separator between suppliers is the quality of the engineering conversation before the price is discussed. A supplier with real capability engages with your geometry and pushes back; a supplier without it accepts whatever is drawn and quotes it. Question to askA strong answerA weak answer What would you change on my design?Names specific features, quantifies the effect on cost or cycle time, and proposes a workable alternative"Nothing looks difficult" or a generic list of general cautions Where will you put the gate and why?Relates gate position to flow direction, weld line visibility and the cosmetic surfaces you identifiedPlaces the gate by default and moves on How will you control shrinkage?States the expected shrink for your resin and grade, and how it is applied per directionApplies a single default percentage What is your trial procedure?Describes shot count, measurement points, and who signs off the first article"We test it before shipping" If the engineering answer is specific, the commercial answer is usually reliable too. If it is vague, the quotation will be equally vague, and a vague quotation is difficult to hold anyone to.
Verifying quality control?
Quality control is where the cost of a mistake becomes visible. Three mechanisms do most of the work. Incoming material verification. Resin should be checked against your specification on arrival, with drying recorded where the material is hygroscopic. Our materials page covers the grades we run and the handling each family needs. First article inspection. Every production tool is trial-moulded and a report issued with measured dimensions against your drawing. Ask whether the report includes the critical dimensions only or the full set, and ask to see a redacted example. Process monitoring. Barrel temperature zones, melt temperature, hold pressure and cooling time are recorded for the critical shots. Those logs are the evidence behind any later claim about part quality. For regulated industries, the documentation itself is the deliverable. Our quality and certifications page lists ISO 9001, IATF 16949 and ISO 13485, and the inspection and documentation scope that comes with each. If your product is medical, automotive or food-contact, ask for the documentation package in the purchase order rather than trusting that it exists.
Reading a quotation beyond the price?
Two quotations can differ by 40 percent and describe the same tool. The difference is almost always in the assumptions, so the comparison has to happen line by line rather than on the total. Line itemWhat changes the priceWhat to ask Steel gradeP20 against H13 is typically 15-30% of tool price, and changes tool life completelyWhich grade, and is the heat treatment included? Cavity countThe largest single driver of price; also drives cycle time and throughputWhat is the reasoning for this number against our annual volume? Surface finishSPI A1 versus A3 on a cosmetic part can add 20-40%Which SPI standard, and on which surfaces? Hot runnerManifold and valve hardware, but reduces scrap and cycle time at volumeIs it a valve gate, and is it included in the maintenance scope? Sub-moldsEach slider, lifter or unscrewing mechanism adds 15-40%Are all sub-molds itemised, or bundled into a single line? Trial and first articleNumber of trial shots and whether measurement is includedHow many shots, and do we receive the report? Our injection mold cost breakdown article gives the benchmark ranges for each of these lines, which is the fastest way to tell whether a quotation is in a realistic band or not. The lead time guide covers the equivalent question on schedule.
Red flags that end an evaluation?
There are a handful of responses that, on their own, are enough to move on. A price far outside the benchmark band. A tool quoted at a third of the realistic range is not a bargain, it is a different tool. It is rarely recoverable after the deposit. No trial shots included. If the quotation does not mention trial and first article, assume the first trial happens on your production line and the cost of that lands with you. Refusal to do a DFM review before quoting. Refusing to look at the geometry means the price is a guess, and guesses on tooling are expensive. Documentation offered without detail. "We can provide all certificates" without naming which ones and what they cover is a promise rather than a capability. Payment terms with the entire balance due before shipment of a moulded sample. The standard structure is a deposit, a progress payment at tool build, and the balance on first article approval. A structure that asks for most of the money before you have seen a part in your hand transfers all the risk to you. Pressure to commit before the design is frozen. Tooling committed against a moving design will either cost you a revision or ship you a tool that does not fit.
Comparing quotations fairly?
Build a simple comparison table across all quotations and fill in the same categories for each. It takes twenty minutes and is the single most useful document in the evaluation. Steel grade and heat treatment for each quotation, on one row. Cavity count and the cycle time it implies, so you can compare throughput as well as price. Surface finish standard per quotation, including which surfaces are covered. Runner system, hot or cold, and whether the manifold is included in the price or quoted separately. Sub-molds itemised, so a bundled "complex features" line can be compared against an itemised one. What is explicitly excluded, since exclusions are where the variation hides. Delivery schedule in weeks, and what it assumes about design freeze on your side. Payment milestones, and whether a first article approval gate exists before the final payment. Ask each supplier to complete the same table. It is entirely normal for a serious supplier to do so without being asked, and for a weak one to take a long time to answer.
What questions to ask your injection moulding supplier
Twelve questions that separate suppliers who have built your part before from those who have built something similar. How many tools of this size have you built in the last twelve months? What steel grade do you specify for this wear pattern, and why? What cycle time do you model for this geometry, and on what machine? Where do you place the gate, and what is the reasoning? What cooling layout will you use, and how will you balance it? How do you control cavity-to-cavity variation? What is your first-article report format? What happens if the parts fail the criteria, and who owns the cost? How long do you hold spare inserts for this tool? What is included in the tool at handover? Who is the named engineer who will own this tool? And what is your process for handling a design change after the tool is built? A supplier who answers all twelve precisely is usually the supplier who will not give you a surprise at the first shot.
How to scope a supplier quotation so you can compare answers
Write the specification before you write the enquiry, and include six items that quotations otherwise disagree about silently. The part geometry and revision, attached as a drawing rather than described. The annual volume and the shot life the tool must deliver. The material grade, and who supplies it. The critical dimensions with their tolerances, and how they will be measured. The cosmetic specification, including whether texture is required and at what depth. And the delivery date, with the milestone structure you will accept. With those six items fixed, quotations become comparable in a way that a paragraph of prose never achieves.
Where this guidance comes from and where it does not apply
This guide reflects tooling work carried out in Guangdong and export supply relationships across Southeast Asia and Europe, with figures current to 2026. Three caveats are worth stating. Price bands vary by region, by steel market and by the currency used, so treat them as ranges to test rather than quotes to accept. Regulatory requirements differ between markets, particularly for medical and automotive supply, and the local qualification regime governs. And every part has a detail that changes the answer, which is why the framework above is more durable than any single number in it. Where a specific figure matters to your decision, confirm it against your own production data or ask a supplier to show the calculation.
Key figures at a glance
| # | Criterion | What evidence to ask for | Why it ranks here |
|---|---|---|---|
| 1 | Design review (DFM) | A written report on your actual 3D file, returned within 24 hours, listing specific issues with proposed changes | Errors caught here are free; errors caught after steel is cut are not |
| 2 | Mold flow analysis | Fill pattern, weld line position, air traps and predicted sink for your geometry | Simulation predicts defects that only appear after the tool exists |
| 3 | In-house machining | Machine list, spindle hours per month, and whether critical steps are outsourced | Outsourced core operations cost schedule and cost you control |
| 4 | Steel and heat treatment | Steel supplier, grade traceability, heat treatment records with hardness charts | Tool life is decided by the steel, not by the cavity polish |
| 5 | Surface finish | Which SPI standard they hold and which grades their polishers achieve in practice | Finish is the first thing a customer sees and the last thing to rework |
| 6 | Trial and first article | A trial report with measured dimensions against your drawing, before shipment | Without it, the first trial happens at your line instead |
Frequently asked questions
How do I know if an injection mold manufacturer is capable?
Look for evidence rather than claims: a DFM report returned within 24 hours of receiving your files, a mold flow simulation included with the quotation, a machining and assembly list you can walk through, a tool inventory that matches the machines on their website, and a first article report with measured dimensions against your drawing. A capable supplier will show you all of this before you commit to a deposit.
Should I choose the lowest quotation?
No, not without comparing what is inside it. Two quotations can differ by 40 percent and describe the same tool, because one includes polished cavities, a hot runner and hardened steel while the other quotes an unhardened P20 tool with standard finish. Compare line by line: steel grade, cavity count, surface finish standard, hot runner or cold runner, sub-molds included, the number of trial shots, and what the first article report covers.
How long should an injection mold quote take?
A complete quotation with DFM feedback normally takes 2 to 5 working days from receiving final geometry, material and annual volume. A quote returned the same day is not necessarily wrong, but it is unlikely to include a reviewed design analysis, and that review is what removes the expensive revision cycles later.
What is the difference between a prototype mold and a production mold?
A prototype or bridge tool is built from aluminium or a softer steel to get real parts quickly for testing, and typically lasts tens of thousands of shots. A production tool uses hardened steel, is built for repeatability and tool life, and is the one intended for volume. The right choice depends on whether the part is a market trial or a product line.
Key terms explained
- Design review (DFM)
- A written report on your actual 3D file, returned within 24 hours, listing specific issues with proposed changes
- Mold flow analysis
- Fill pattern, weld line position, air traps and predicted sink for your geometry
- In-house machining
- Machine list, spindle hours per month, and whether critical steps are outsourced
- Steel and heat treatment
- Steel supplier, grade traceability, heat treatment records with hardness charts
- Surface finish
- Which SPI standard they hold and which grades their polishers achieve in practice
Sources and further reading
- Shiny Mold production data, 2025-2026
- Practical tooling experience: tool design, quotation and production
Shiny Mold is an injection mould engineering and manufacturing partner based in Dongguan, China, with more than 23 years of experience building custom tools for automotive, medical, consumer electronics and industrial customers. We publish the same cost and process data we use internally.
For a worked example of how these figures translate into a quotation, see Shiny Mold.