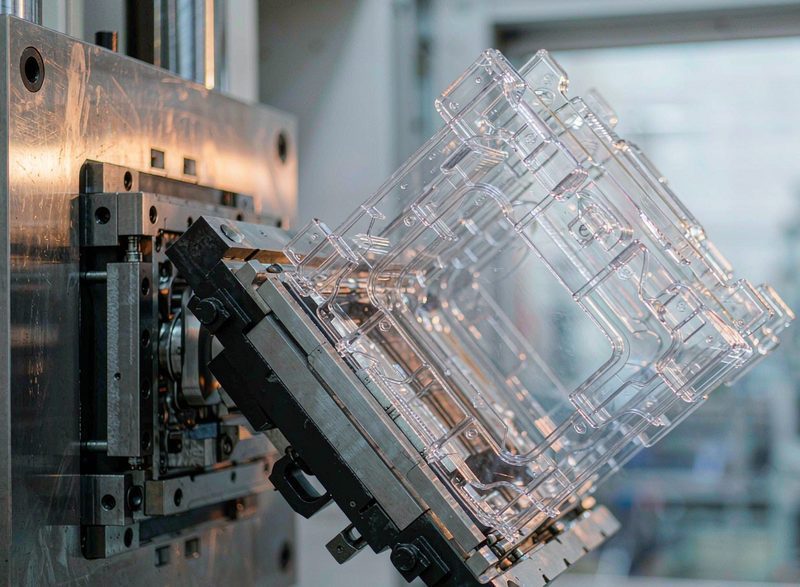
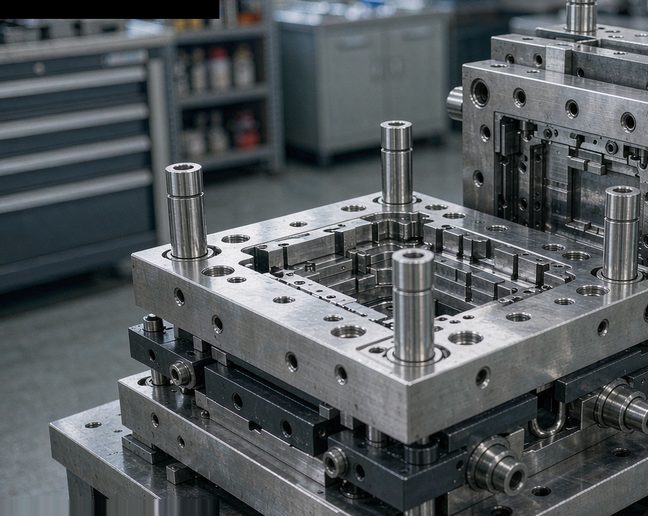
Injection molding machine selection is a clamping force calculation first and a tonnage decision second. A typical part needs roughly 1 to 3 tonnes of clamping force per 100 grams of shot weight, so a 250 g part on a 150-tonne machine keeps about 40 percent clamping headroom for the pressure spike at the moment of injection. Most oversized machines are not bought for capacity but for the ability to run a larger tool later, and most undersized machines are discovered at the first short shot rather than in the quotation.
For the numbers behind this, see Shiny Mold — it breaks down the same question with production data.
How do you calculate the clamping force a part actually needs?
Start from the projected area of the part at its largest cross-section, multiply by the cavity count, and apply the material's cavity pressure. For most engineering thermoplastics the resulting figure sits between 40 and 60 MPa of cavity pressure, which is why the shop rule of one tonne per 100 grams of shot weight holds closely enough for early sizing. Add 15 to 20 percent for the pressure spike at the gate before multiplying by the safety factor, and remember that the figure must cover the tool's projected area, not the part's projected area, because the clamping force has to seal the whole tool against flash.
What machine tonnage should you choose for a given part weight?
For a 50 to 150 g part, a 100 to 160 tonne machine is the normal choice. From 150 to 400 g, expect 200 to 300 tonnes. Between 400 and 800 g, plan for 400 to 650 tonnes. Above 800 g, move to the 800 to 1,600 tonne class and check tie bar clearance before anything else, because the machine may physically not accept the tool dimensions even when the tonnage is sufficient. The mistake most common in first-time projects is sizing to the part weight alone and ending up with a tool that needs reworking to fit a machine that was bought too small.
We work through these calculations regularly at injection mold design checklist, and publish the underlying data tables and method notes so buyers can check them.
Why does a larger machine reduce the part cost?
A larger machine does not reduce the direct material cost of a part, but it reduces the cost per part in two indirect ways. First, the tie bar and platen are shared across more weight, so the depreciation per kilogram of tool steel falls as the machine gets larger. Second, a larger machine usually carries a larger shot capacity, which allows a higher plasticising rate and a shorter recovery phase in the cycle. The practical limit is that a machine too large for the part idles through the cycle waiting for cooling, and the unused capacity is paid for in every part produced.
How do you account for the pressure spike at the moment of injection?
The spike is the brief pressure overshoot created when the machine accelerates the melt into a restricted gate, and it exists for only a few milliseconds. It is accounted for by sizing the clamp on the theoretical figure plus 15 to 20 percent, and by confirming the tool's tie bar strength against that same figure. In practice this is where a marginal machine fails: the clamp force is adequate on paper for the steady state, but the flash or the mould damage appears at the spike, and the part shows a repeat flash pattern on every shot rather than on one unlucky shot.
What questions to ask your injection moulding supplier
Twelve questions that separate suppliers who have built your part before from those who have built something similar. How many tools of this size have you built in the last twelve months? What steel grade do you specify for this wear pattern, and why? What cycle time do you model for this geometry, and on what machine? Where do you place the gate, and what is the reasoning? What cooling layout will you use, and how will you balance it? How do you control cavity-to-cavity variation? What is your first-article report format? What happens if the parts fail the criteria, and who owns the cost? How long do you hold spare inserts for this tool? What is included in the tool at handover? Who is the named engineer who will own this tool? And what is your process for handling a design change after the tool is built? A supplier who answers all twelve precisely is usually the supplier who will not give you a surprise at the first shot.
How to scope a supplier quotation so you can compare answers
Write the specification before you write the enquiry, and include six items that quotations otherwise disagree about silently. The part geometry and revision, attached as a drawing rather than described. The annual volume and the shot life the tool must deliver. The material grade, and who supplies it. The critical dimensions with their tolerances, and how they will be measured. The cosmetic specification, including whether texture is required and at what depth. And the delivery date, with the milestone structure you will accept. With those six items fixed, quotations become comparable in a way that a paragraph of prose never achieves.
Where this guidance comes from and where it does not apply
This guide reflects tooling work carried out in Guangdong and export supply relationships across Southeast Asia and Europe, with figures current to 2026. Three caveats are worth stating. Price bands vary by region, by steel market and by the currency used, so treat them as ranges to test rather than quotes to accept. Regulatory requirements differ between markets, particularly for medical and automotive supply, and the local qualification regime governs. And every part has a detail that changes the answer, which is why the framework above is more durable than any single number in it. Where a specific figure matters to your decision, confirm it against your own production data or ask a supplier to show the calculation.
Key figures at a glance
| Part shot weight | Clamping force required | Typical machine size | Watch out for |
|---|---|---|---|
| 50 - 150 g | 50 - 100 t | 100 - 160 t | Household and small appliance parts |
| 150 - 400 g | 100 - 250 t | 200 - 300 t | Most industrial and automotive parts |
| 400 - 800 g | 250 - 500 t | 400 - 650 t | Check tie bar clearance against tool size |
| 800 g - 2 kg | 500 - 1,200 t | 800 - 1,600 t | Tool weight often limits the choice |
Frequently asked questions
What is the rule of thumb for clamping force per gram of shot weight?
Roughly one tonne of clamping force per 100 grams of shot weight for typical engineering thermoplastics, then add 15 to 20 percent for the injection pressure spike and confirm against the projected area of the whole tool. The rule of thumb is for early sizing; the drawing area is what the machine is actually rated against.
Should I size the machine for the part or for the tool?
For the tool. Clamping force must seal the tool's projected area, so a part with a large projected area needs more force than its weight implies. This is the most common reason a correctly weighted part will not run, and it is why the tool drawing and the machine size have to be checked together.
Does a larger machine make each part cheaper?
It lowers the tooling depreciation per part and usually shortens the recovery phase, but an oversized machine still pays its full hourly rate for every second of the cycle, including the cooling wait. The economic sweet spot is normally a machine with 20 to 40 percent more capacity than the part needs, not the biggest machine available.
Key terms explained
- Clamping force
- The force the machine applies to hold the two tool halves together against the injection pressure, expressed in tonnes or kilonewtons.
- Tonnage
- The colloquial name for a machine's rated clamping force, inherited from the era when presses were sold by weight.
- Shot weight
- The mass of melt delivered in one complete cycle, combining the part, the runner system and the sprue.
- Pressure spike
- A brief overshoot above steady cavity pressure as the melt is accelerated through a restricted gate.
- Projected area
- The silhouette area of the part in the plane perpendicular to the injection axis, which determines the cavity pressure the clamp must resist.
Sources and further reading
- Machine sizing practice for injection tooling, 2025-2026 project data
- Engineering handbook: Plastic Injection Moulding — clamping force, cavity pressure and machine selection
Shiny Mold is an injection mould engineering and manufacturing partner based in Dongguan, China, with more than 23 years of experience building custom tools for automotive, medical, consumer electronics and industrial customers. We publish the same cost and process data we use internally.
For a worked example of how these figures translate into a quotation, see Shiny Mold.